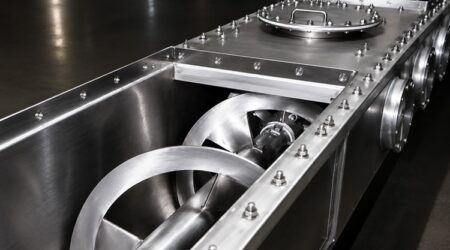
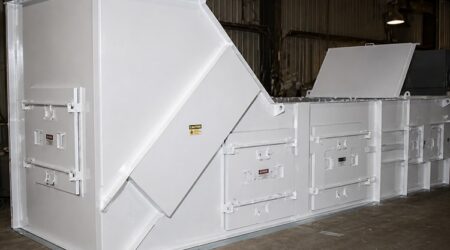
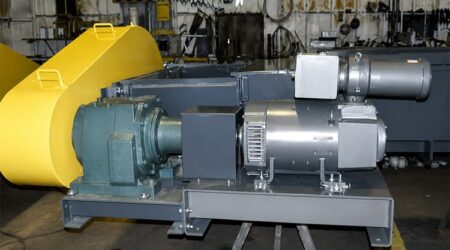
A leading pet food manufacturer needed a large-scale conveying solution for two production facilities, with approximately 250 screw conveyors, feeders, and live bin bottoms engineered and delivered on overlapping schedules.
Continue Reading
BW Sinclair
A leading pet food manufacturer needed a large-scale conveying solution for two production facilities, with approximately 250 screw conveyors, feeders, and live bin bottoms engineered and delivered on overlapping schedules.
A Midwestern petrochemical manufacturer needed to expand production of a proprietary crystalline product and required a complete upgrade to the discharge system between four centrifuges and a downstream rotary dryer. B.W. Sinclair Inc. designed and fabricated a totally enclosed system...
An East Coast cane sugar refinery required replacement of two primary sugar minglers that had been in service since the 1920s. B.W. Sinclair Inc. designed and fabricated modern, heavy-duty mingler units that preserved the original process function while incorporating current...
A major food processor required an advanced screw conveyor system capable of simultaneously conveying, mixing, and parboiling wild rice under low-pressure saturated steam conditions. B.W. Sinclair Inc. designed and fabricated a pair of custom tubular screw conveyors engineered specifically for...
A major distributor of fine granular soda ash required a compact, high-capacity system to transfer product from railcars to trucks at a Pennsylvania transportation hub. B.W. Sinclair Inc. designed and installed a 90° Z-Flow Vertical Flexible Sidewall Belt Conveyor delivering...
One of the nation's leading cement producers required a reliable feeding solution to meter synthetic gypsum into their manufacturing process. After reviewing B.W. Sinclair's design and operational approach, the client specified four BWSI multi-screw Live Bottom Feeders, engineered specifically for...
From sticky and abrasive materials to high-capacity conveying systems, we build equipment that performs where standard solutions fail.
Contact Us Today