A Midwestern petrochemical manufacturer needed to expand production of a proprietary crystalline product and required a complete upgrade to the discharge system between four centrifuges and a downstream rotary dryer. B.W. Sinclair Inc. designed and fabricated a totally enclosed system to collect, contain, and meter the moist crystalline discharge — addressing sanitation, product purity, material adhesion, and environmental containment requirements in a single integrated solution.
The Challenge
Moist crystalline powders present some of the most difficult bulk material handling challenges. This application involved:
- Material adhesion. The moist product adhered to equipment surfaces, causing buildup and flow restriction.
- Bridging and packing. The material's cohesive properties made reliable discharge from bins problematic.
- Sanitation requirements. All product-contact surfaces required a specific surface finish for sanitary compliance and material release.
- Environmental containment. A totally enclosed system was required to prevent emissions.
- Process integration. The system needed to accept discharge from four separate centrifuges and meter the combined flow uniformly into the dryer barrel.
Our Solution
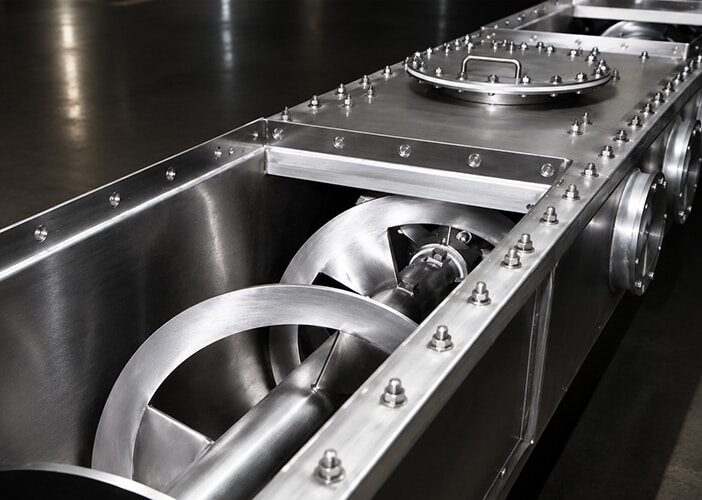
B.W. Sinclair designed a two-component system: triple-screw live bottom bins to collect centrifuge discharge and prevent bridging, feeding into a transfer screw conveyor that meters product directly into the rotary dryer.
Component 1: Live Bottom Bins
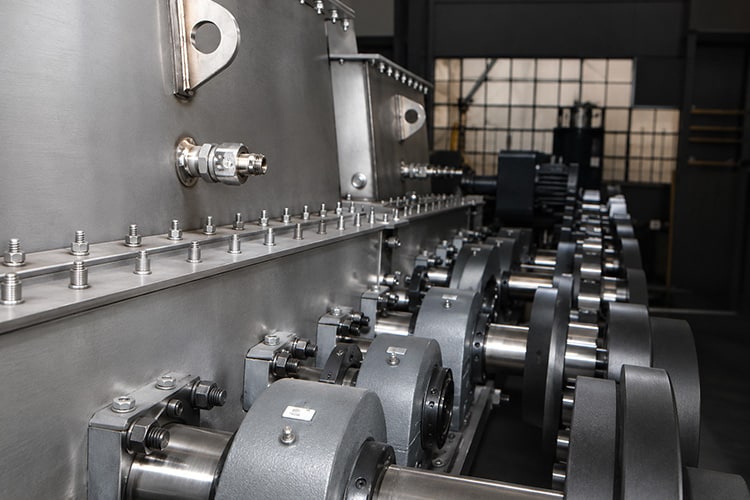
- Model: 0216-3-LBB, 16-inch diameter Triple-Screw Live Bottom Bins
- Construction: All T304L stainless steel
- Hopper Design: Negative Sidewall surge hoppers. Prevents bridging and packing of adhesive material.
- Screw Design: Ribbon flight variable-pitch feeder screws. Prevents material adhesion to screw surfaces.
The triple-screw live bottom configuration provides large-area, even withdrawal across the full hopper cross-section, eliminating the bridging and channeling common in single-discharge hoppers handling cohesive or moist powders.
Component 2: Transfer Screw Conveyor
- Model: 0124-SS, 24-inch diameter Transfer Screw Conveyor
- Construction: All T304L stainless steel
- Screw Design: Ribbon flight full-pitch screws
- Discharge: Final cantilevered helix for direct injection into rotary dryer barrel
The cantilevered discharge helix extends into the dryer inlet, ensuring a controlled, uniform material stream enters the dryer barrel and preventing pulse loading that would reduce dryer efficiency.
Key Engineering Features
Every component was specified to address the specific handling challenges of moist, adhesive crystalline powder:
- Woodex-MECO™ nitrogen-purged elastomer gland seals at all shaft penetrations. Provides a positive pressure barrier against product escape and atmospheric contamination, critical for environmental containment and product purity.
- BWSi SIN-7 surface finish (120-140 grit) on all product-contact areas. Promotes material release and simplifies sanitary cleaning, reducing adhesion-related maintenance.
- Pedestal-mounted spherical roller bearing pillow blocks for robust shaft support isolated from product contact areas.
- Glass-filled Teflon® internal support bearing on Transfer Screw. A self-lubricating bearing compatible with the crystalline product; eliminates external lubrication requirements in the product stream.
- Special floating joint between Live Bottom Bins and Transfer Screw. Accommodates differential thermal expansion between components without binding or misalignment.
- Product conveyability testing at BWSi factory prior to final engineering, witnessed by client and consultant. Confirms the handling solution before fabrication commitments are made.
- Initial startup assistance and operator training to ensure proper commissioning and consistent operation from day one.
Result
B.W. Sinclair delivered a totally enclosed, sanitary-grade discharge and transfer system that solved every identified material handling challenge. The negative sidewall hoppers, ribbon flight screws, nitrogen-purged seals, and specified surface finish work together to ensure reliable flow, clean operation, and environmental containment — enabling the client's production expansion without compromise on purity or process control.
Hard-to-Handle Materials? That's Our Specialty.
B.W. Sinclair designs and fabricates custom live bottom bins, screw feeders, and conveying systems for the most difficult bulk material handling applications — moist powders, adhesive granules, bridging-prone solids, and materials that defeat standard equipment. Contact our engineering team to discuss your application.
Equipment Used
Live bottom bins, transfer screw conveyor