A major food processor required an advanced screw conveyor system capable of simultaneously conveying, mixing, and parboiling wild rice under low-pressure saturated steam conditions. B.W. Sinclair Inc. designed and fabricated a pair of custom tubular screw conveyors engineered specifically for the thermal, sanitary, and process control demands of this food-grade application.
The Challenge
Standard conveying equipment cannot perform in-process steam treatment of bulk food materials. The client needed a system that could:
- Introduce low-pressure saturated steam uniformly along the conveyor length
- Provide several minutes of controlled retention time for thorough parboiling
- Collect and drain condensate to prevent product contamination
- Accommodate significant thermal expansion during steam operation
- Meet food-grade sanitary standards throughout all product-contact surfaces
The B.W. Sinclair Solution
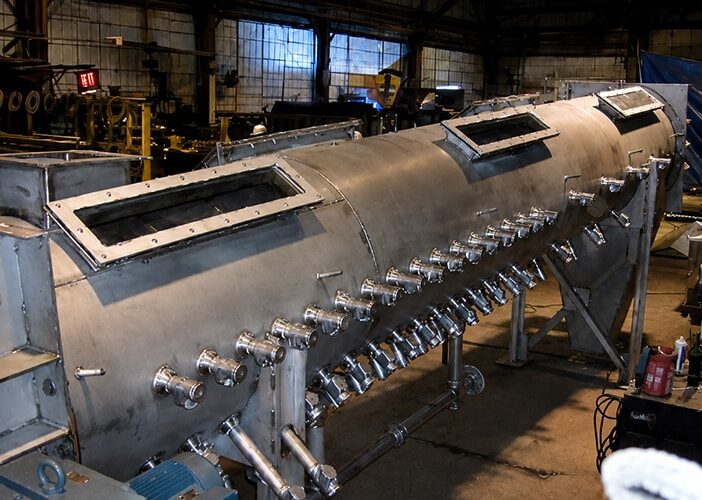
B.W. Sinclair engineered a pair of 36-inch diameter LongSpan™ tubular screw conveyors in all Type 304-L stainless steel construction. The rotors feature reduced-pitch flights and mixing paddles specifically designed to retard material transfer and promote uniform mixing — extending retention time to the client's process specification.Steam Injection System
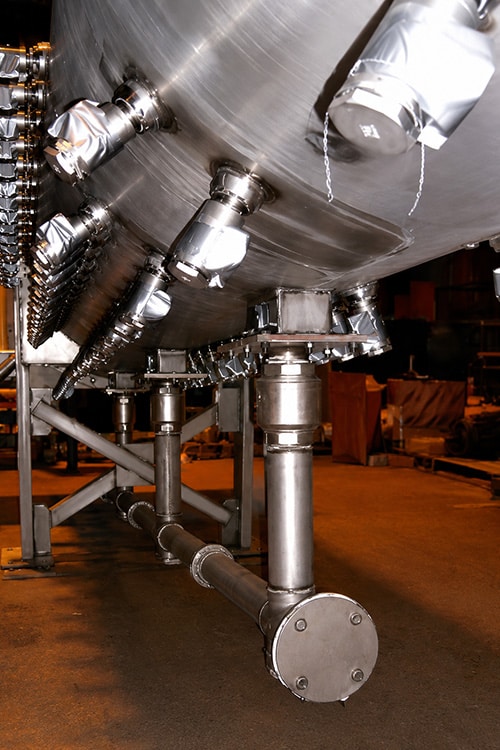
Steam is introduced through a series of multiple nozzles, each fitted with flexible tubing to accommodate thermal expansion. The nozzles are eccentrically positioned along the conveyor barrel to concentrate steam delivery precisely where the client's process requires it.
Condensate Management
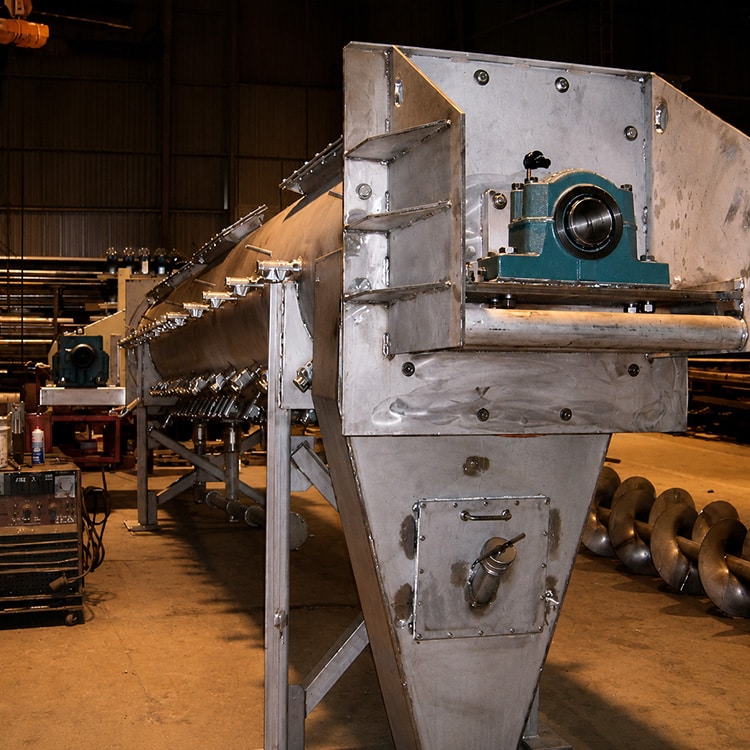
A series of individually controllable condensate collection ports, mounted on the lower centerline of each conveyor, collect and drain process liquids to a central takeoff. Individual port control provides maximum flexibility as throughput rates or steam pressure varies.
Key Engineering Features
B.W. Sinclair incorporated specialized components to address every aspect of this demanding food processing application:
- Cinchseal™ silicone elastomer purged gland seals with thermal expansion capability — preventing steam or product escape at shaft penetrations
- BWSI Expansion-Pedestal Bearing Mount — accommodates unequal thermal growth between rotor and trough under live steam conditions
- Dodge SAF-XT™ spherical roller bearing pillow blocks — robust rotor support rated for elevated temperatures
- Polycarbonate view windows in rectangular inspection ports — allows visual process monitoring without opening the unit
- Multiple instrument connection ports — accommodates client's process monitoring instrumentation
- Integral support stanchions — simplifies installation and alignment in the plant layout
- Sealed cleanout and access door with tubular 'poke port' on discharge spout — enables clearing of downstream blockages without full shutdown
- High-efficiency Dodge Quantis™ gearmotor with roller chain primary drive — provides the slow-speed, high-torque operation required for mixing duty
- Inverter-rated Reliance Electric® motor — allows infinitely variable speed adjustment to dial in retention time
- Fine-mesh screens at all steam inlets and condensate drains — prevents product intrusion into process connections
Materials & Construction
Trough & Rotor Material: All Type 304-L stainless steel
Rotor Diameter: 36 inches (LongSpan™ design)
Rotor Configuration: Reduced-pitch flights with mixing paddles
Sealing System: Cinchseal™ purged elastomer gland seals
Drive System: Dodge Quantis™ gearmotor, roller chain primary, inverter-rated motor
Steam Connections: Multiple nozzles with flexible tubing, fine-mesh filtered inlets
Condensate System: Individually controlled lower-centerline drain ports
Result
B.W. Sinclair delivered a fully integrated parboil conveyor system that met every process requirement — precise retention time, consistent steam distribution, reliable condensate removal, and sanitary construction throughout. The system replaced a legacy conveying process while adding in-line thermal treatment capability, reducing handling steps and improving process control.Engineered for Your Application
Engineered for Custom Applications
B.W. Sinclair designs and fabricates custom screw conveyors for difficult food processing, chemical, and industrial applications. If your process involves difficult materials, tight retention time requirements, or integrated thermal treatment, contact our engineering team to discuss your application.
Equipment Used
Screw Conveyors and Feeders, Custom Applications