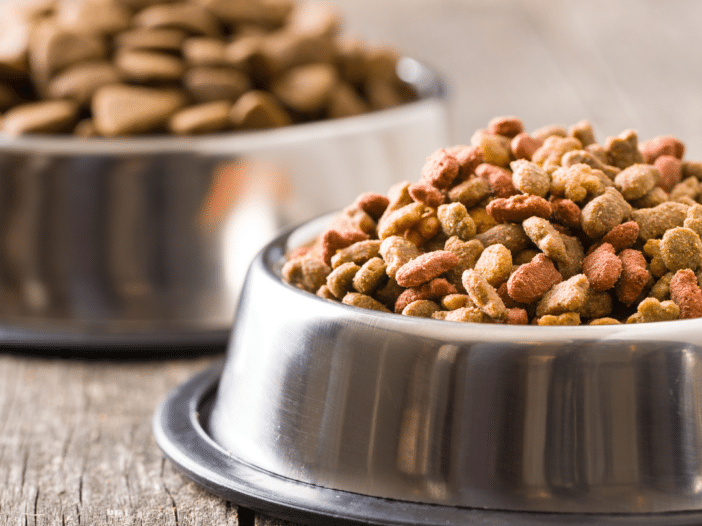
Material Handled: Various dry ingredients used in pet food production
Equipment Supplied: Approximately 250 conveying units, including conveyors, feeders, and live bin bottoms
Application: Ingredient handling and production feeding across two manufacturing facilities
Challenge
A leading pet food manufacturer needed a large-scale conveying solution for two production facilities being constructed and commissioned on overlapping schedules. The project included approximately 250 pieces of material-handling equipment, consisting of screw conveyors, screw feeders, and live bin bottoms, all of which had to be engineered, manufactured, and delivered within a demanding project timeline.
In addition to the scale and scheduling requirements, the conveying systems needed to handle a variety of ingredients used throughout the pet food production process. Because individual feeders and live bin bottoms could encounter different materials at different stages of production, some units needed to accommodate multiple conveying rates and operating conditions.
Operator safety and sanitary equipment design were also major considerations throughout the engineering process. The equipment needed to minimize areas where material could collect, remain stagnant, or create potential sanitation concerns.
Solution
BW Sinclair engineered the conveying equipment around the specific process requirements of each location while also looking for opportunities to standardize components across the project.
For equipment that would handle multiple ingredients, conveyors, feeders, and live bin bottoms were designed to operate across the required range of material characteristics and conveying rates. Additional engineering was also incorporated at certain feeder inlets to provide the structural support required for the application.
Sanitary design was considered throughout the equipment. Potential material hang-up points were evaluated and minimized, including the use of welded-in bolts and other design modifications where needed to eliminate areas where product could accumulate. Operator safety requirements were incorporated into each conveyor, with the appropriate guarding and safety provisions included as part of the overall equipment design.
With such a large number of units being installed across two facilities, BW Sinclair also designed the equipment to use as many common components and spare parts as practical. This standardization reduced the number of unique replacement parts the customer would need to keep in inventory and simplified long-term maintenance across both plants.
Result
BW Sinclair successfully engineered and supplied the equipment for both facilities while meeting the project’s required milestones and delivery deadlines.
The completed systems provided the flexibility needed to handle multiple pet food ingredients and conveying rates while addressing the customer’s requirements for operator safety, sanitation, structural support, and maintainability.
By standardizing components wherever possible, BW Sinclair also helped reduce the customer’s spare-parts inventory requirements across the two plants, providing a conveying solution designed not only for successful startup, but also for efficient long-term operation and maintenance.
Equipment Used
Screw Conveyors and Feeders