An East Coast cane sugar refinery required replacement of two primary sugar minglers that had been in service since the 1920s. B.W. Sinclair Inc. designed and fabricated modern, heavy-duty mingler units that preserved the original process function while incorporating current engineering standards for reliability, seal integrity, and process flexibility.
Understanding the Application
In cane sugar refining, a mingler is a critical piece of process equipment used to combine raw sugar crystals with affination syrup. This wet mixing step initiates the transformation from raw cane sugar into refined granulated product. The process demands:
- Intense, thorough mixing of viscous sugar slurry at controlled rotational speed
- Extended retention time to allow proper affination before downstream processing
- Containment of highly viscous slurry to prevent premature discharge
- Adjustable weir height to manage product viscosity across variable throughput rates
- Continuous visual access for process monitoring without interrupting production
The B.W. Sinclair Solution
B.W. Sinclair engineered a dual-rotor design that provides thorough mixing through two complementary mechanical actions within a single 36-inch U-trough housing. The inner helix moves material axially while the outer paddle rotor provides radial and cross-directional mixing, ensuring uniform slurry composition at slow, controlled rotational speed.
Dual-Rotor Configuration
Inner Rotor: 24-inch diameter sectional flight helix. Provides axial material movement.
Outer Rotor: 30-inch diameter reverse paddle rotor. Provides cross-mixing and retention.
Trough: 36-inch U-trough with discharge bulkhead and adjustable weir
Construction: Heavy seal-welded carbon steel (stainless not required at this process stage)
Retention Time Control
A discharge bulkhead and weir arrangement prevents viscous slurry from evacuating the trough prematurely. The weir height is field-adjustable, allowing operators to tune retention time across a range of volumetric production rates — a critical feature when sugar crystal size or syrup viscosity varies by batch.
Process Visibility
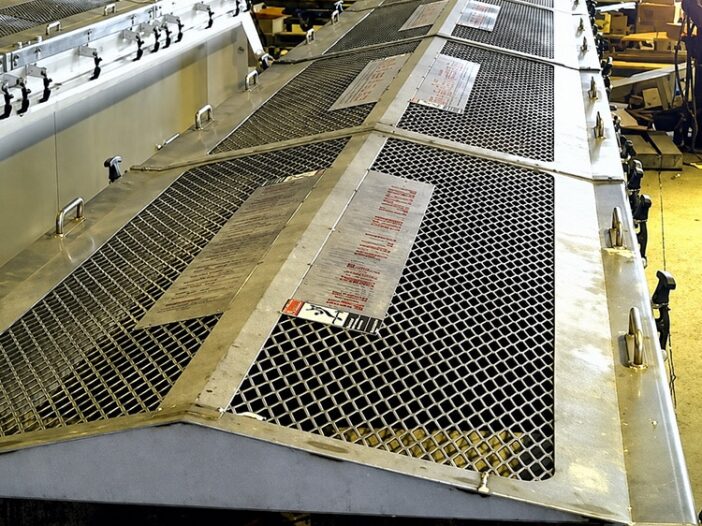
Reinforced stainless steel mesh clamped top covers run the full length of the minglers, allowing continuous visual inspection of the mixing process without opening the unit or interrupting production.
Key Engineering Features
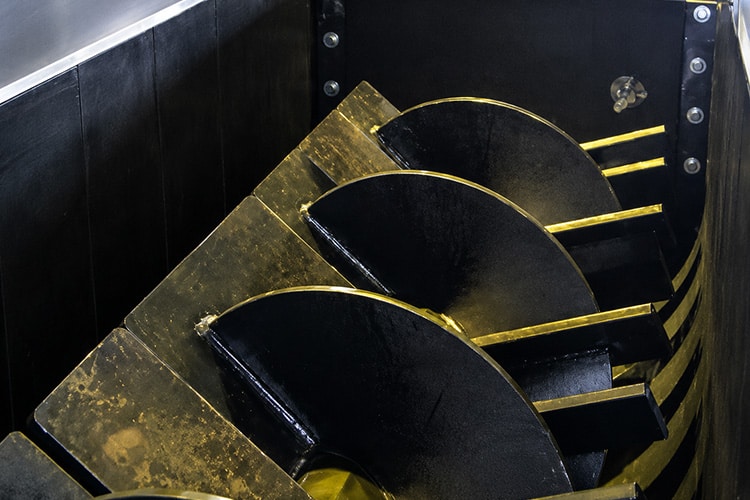
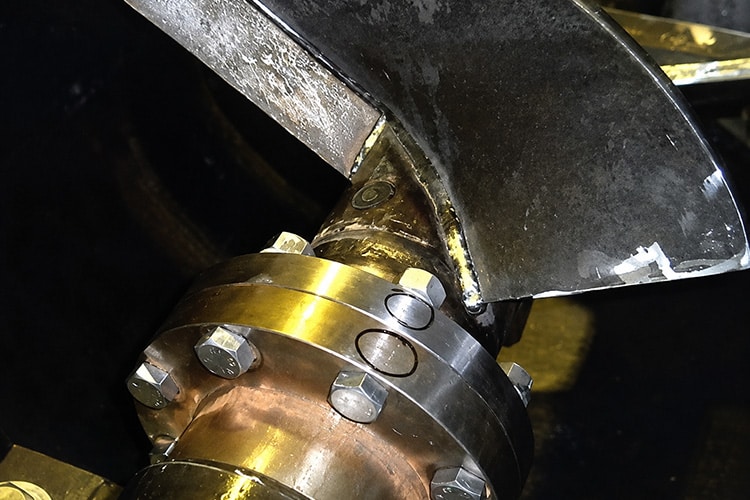
- Flanged rotors with body-bound coupling bolts for precise rotor alignment under heavy torque loads.
- Super heavy-duty intermediate free-flow hanger frame with machined bronze support bearing. Sustains high rotor loads across long spans without deflection.
- Double offset side-mounted discharge spouts for flexible discharge routing to match existing plant layout.
- Adjustable packing gland shaft seals with Teflon™ braided packing. Field-serviceable sealing for viscous slurry applications.
- Dodge SAF-XT™ spherical roller bearing pillow blocks. Heavy-duty shaft support rated for high radial and thrust loads.
- Falk Quadrive™ flange-mounted helical gear drive. Delivers the high-torque, low-speed operation required for dense slurry mixing.
- Inverter-duty Marathon Blue-Chip™ motor for variable speed control and process optimization.
Result
The two B.W. Sinclair minglers replaced equipment that had been in continuous service for nearly a century, bringing the refinery's front-end slurry mixing process into compliance with current engineering standards. The adjustable weir system, dual-rotor mixing action, and heavy-duty mechanical components provide process flexibility and reliability that aging legacy equipment could not match.
Engineered for Your Process
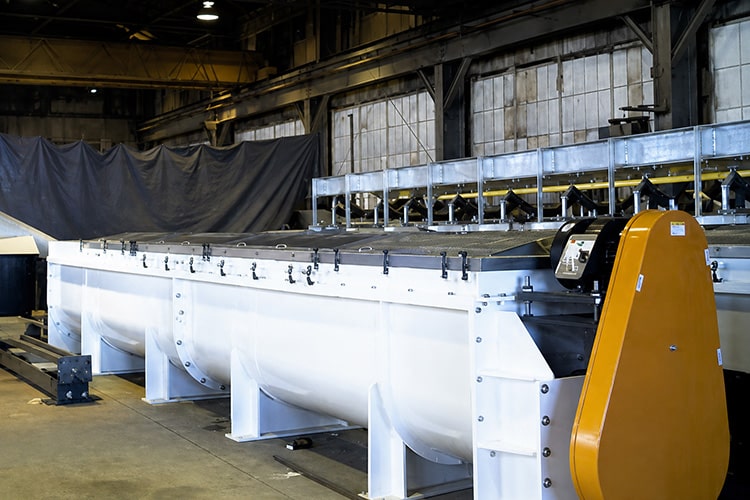
B.W. Sinclair designs and fabricates custom screw conveyors and mixing equipment for food, chemical, and industrial applications, including retrofit replacements for aging process equipment. Contact our engineering team to discuss your application.
Equipment Used
Screw Conveyors and Feeders, Custom Applications