About BW Sinclair
Built on Decades of Experience
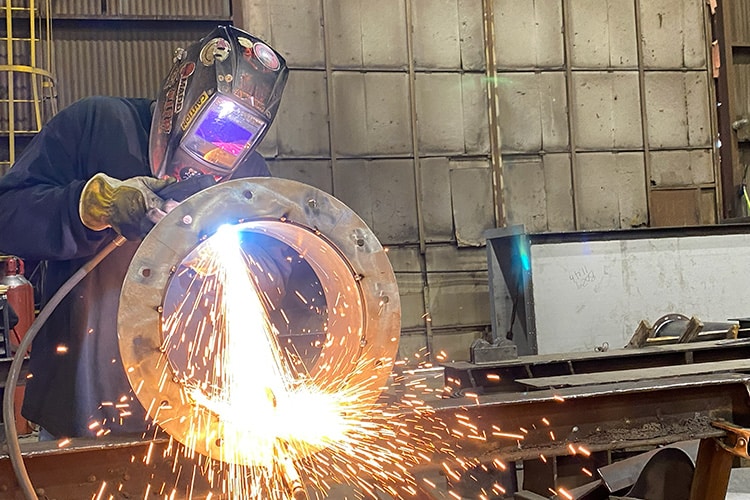
Since 1985, B.W. Sinclair has been designing and manufacturing custom bulk material handling equipment for some of the world’s most demanding industries. From moving sticky materials like peanut butter and TiO₂ to handling abrasive aggregates and heavy ore, our engineered solutions are built to perform where reliability matters most. With decades of experience across a wide range of applications, we understand that every process is unique and every system must be designed with performance, durability, and efficiency in mind.
Our Mission
Our mission is to help customers move bulk materials with confidence by delivering reliable equipment, responsive service, and solutions built around real-world applications. We are committed to doing business with integrity, standing behind our work, and building lasting partnerships through quality, accountability, and trust.

A Trusted Partner for Every Project
For nearly four decades, Fortune 100 manufacturers, EPC firms, and growing businesses have trusted B.W. Sinclair to deliver dependable material handling solutions that stand the test of time. Our complete line of equipment, including bucket elevators, belt conveyors, screw conveyors, feeders, slide gates, and diverter valves, is engineered to integrate seamlessly into your operation and support long-term productivity. Whether you’re replacing a single piece of equipment or designing a complete material handling system, our team is committed to responsive service, quality craftsmanship, and practical engineering solutions. We take pride in building lasting relationships by delivering reliable equipment, clear communication, and the flexibility to meet the unique needs of every customer, regardless of project size.