A western building materials manufacturer required a complete material handling system to transfer run-of-mine gypsum ore from the quarry truck dump station through crushing and into the storage silos above the wallboard pin mixers. B.W. Sinclair Inc. designed, fabricated, and commissioned the full system as a single-source contractor, managing every stage from initial equipment engineering through on-site startup.
The Challenge
Gypsum ore handling from quarry to finished-product storage involves multiple elevation changes, particle size transitions, and dust containment requirements across two separate buildings. The client needed a single contractor to coordinate the complete system rather than managing multiple equipment vendors independently. Key requirements included:
- Receive and feed run-of-mine ore (up to 12 inches) from truck dump directly into the crusher building
- Elevate and meter ore through primary crushing in a dust-controlled enclosure
- Distribute crushed stone across multiple stockpile bunkers automatically
- Transfer pulverized gypsum between the crushing and manufacturing buildings across a 100-foot span
- Deliver the finished material to storage silos above the pin mixers for wallboard production
The Solution
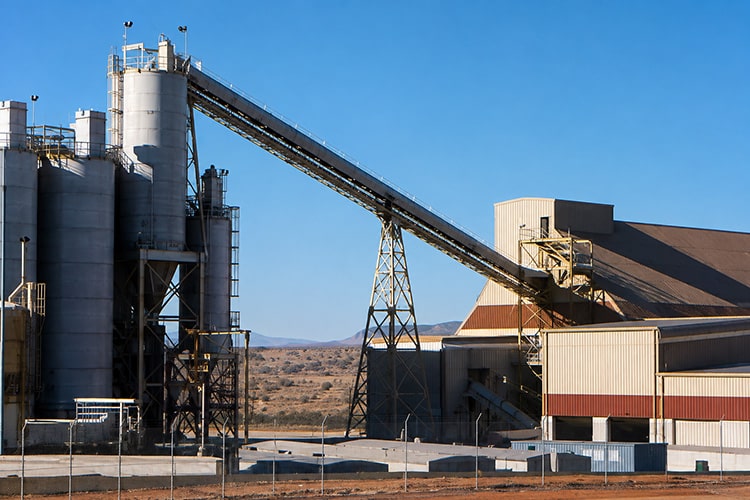
B.W. Sinclair supplied an integrated five-stage system covering the full material flow path from truck dump to silo. Each stage was engineered as part of a coordinated whole, with controls, structural supports, and transitions designed for compatibility across every handoff point.
Stage 1: Truck Dump and Primary Feed
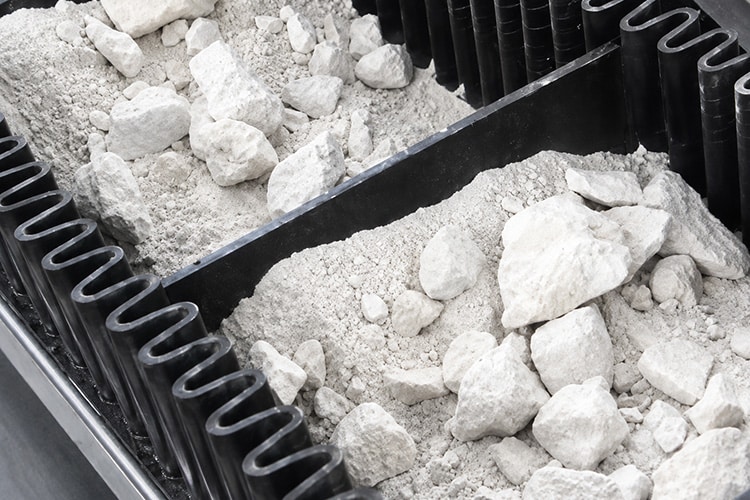
A Truck Dump Hopper and Volumetric Belt Feeder at the back end of the crusher building receive run-of-mine ore directly from quarry haul trucks. The volumetric feeder meters material into the system at a controlled rate, protecting downstream equipment from surge loading.
Stage 2: High-Incline Elevation to Crusher Tower
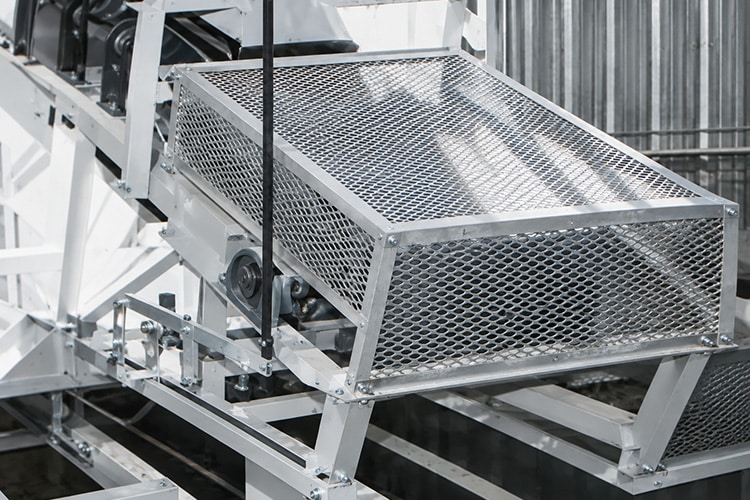
A High-Incline Flexible Sidewall Belt Conveyor elevates the run-of-mine ore from the truck dump level to the crusher tower inlet. An Eriez SP™ suspended permanent magnetic separator, mounted on a custom trolley for periodic manual cleaning, removes tramp iron from the ore stream before it enters the crushers.
Stage 3: Mill-Duty Bucket Elevator
From the crushers, ore drops to a BWSI Model 900™ Mill-Duty Centrifugal Discharge Bucket Elevator fitted with Style AC high-capacity buckets. The heavy-duty seal-welded, dust-tight casing contains the dusty crushed material as it climbs to the top of the crushing building. A BWSI Model 1000 two-way pneumatic diverter valve at the elevator head routes the crushed material either to stockpile or directly to the wallboard mill.
Stage 4: Automatic Tripper Distribution
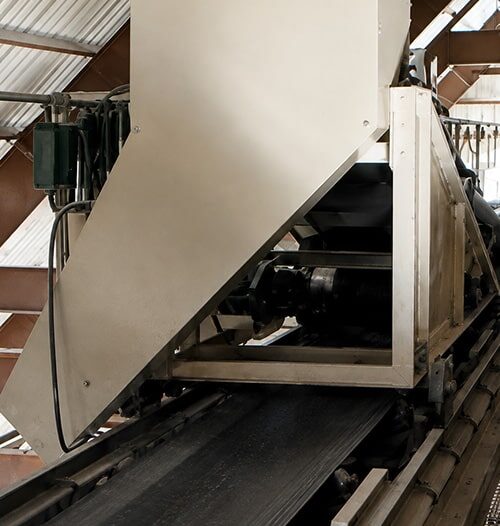
A Horizontal Distribution Belt Conveyor with a powered Tripper Module distributes crushed stone across multiple bunker stockpile locations. The automatic tripper responds to position-indicating limit switches, stopping at pre-selected locations to deposit material into the correct bunker without operator intervention.
Stage 5: Cross-Building Transfer Belt
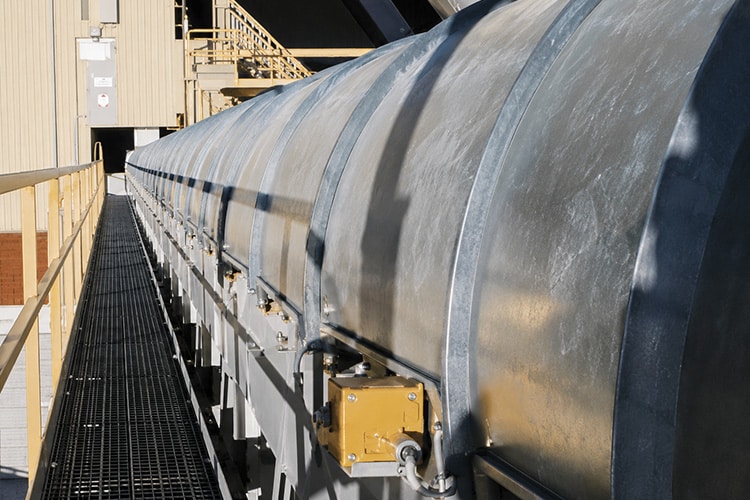
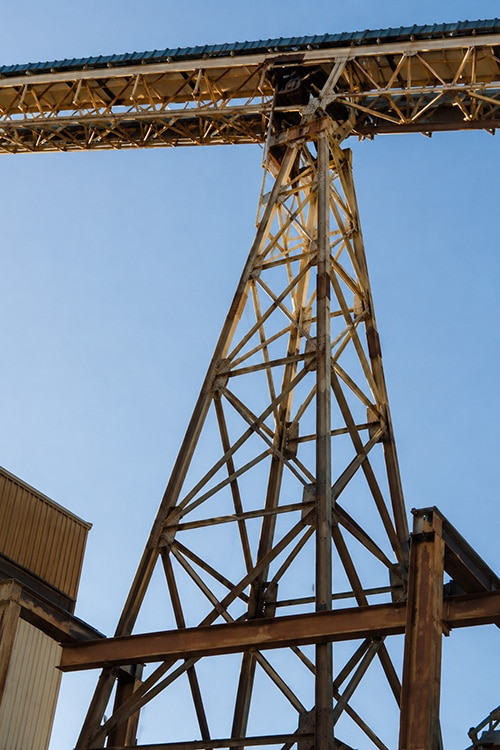
An Inclined Belt Conveyor transfers pulverized gypsum between the crushing and manufacturing buildings, where it becomes the core material in wallboard sheet production. The belt spans approximately 100 feet between supports on a custom structural steel truss, with belt tension maintained by a BWSI three-pulley gravity take-up system integrated into the central support tower.
Equipment Summary
- Truck Feed: Truck Dump Hopper with Volumetric Belt Feeder
- Primary Elevation: High-Incline Flexible Sidewall Belt Conveyor
- Tramp Iron Removal: Eriez SP™ Suspended Permanent Magnetic Separator on custom trolley
- Vertical Elevation: BWSI Model 900™ Mill-Duty Centrifugal Discharge Bucket Elevator, Style AC buckets
- Material Routing: BWSI Model 1000 Two-Way Pneumatic Diverter Valve
- Stockpile Distribution: Horizontal Distribution Belt Conveyor with powered Tripper Module
- Cross-Building Transfer: Inclined Belt Conveyor, ~100 ft span, custom structural steel truss, three-pulley gravity take-up
The Result
We delivered the complete integrated system on time and on budget. Single-source responsibility allowed the client to work with one engineering and fabrication partner across all five system stages, eliminating the interface coordination risk that comes with managing multiple equipment vendors. System startup and commissioning were completed without delays.
Contact Us For Integrated Bulk Material Handling Systems
B.W. Sinclair designs and fabricates complete bulk material handling systems for mining, building materials, chemical, and industrial applications. From single equipment pieces to fully integrated multi-stage systems, contact our engineering team to discuss your project.
Equipment Used
Flexible Sidewall Conveyors, Bucket Elevators, Belt Conveyors and Feeders, Diverter Valves and Slide Gates